What evidence should suppliers provide for color consistency across batches?
For B2B buyers in the toy and educational-products space, color consistency is not cosmetic only — it affects brand integrity, consumer safety, and regulatory compliance. Clear, measurable evidence from suppliers reduces rework, rejects, and brand risk across global distribution channels.
Why color evidence matters for toy importers
Buyers sourcing educational toys — from screen-free OID reading pens and talking flash-card machines to water doodle mats and wearable anime badges — operate in a high-volume, high-scrutiny industry. The global educational toy market is projected to reach $34.5 billion by 2028 (Grand View Research), and China exports over $38 billion in toys annually (China Customs). In this environment, buyers must treat color control as a technical deliverable backed by data and traceability.
Business and safety reasons to demand evidence
- Brand consistency: unmatched shades damage shelf appeal and retailer relationships.
- Regulatory & chemical safety: pigment chemistry links to EN71/CPSIA/REACH compliance and parent concerns — 73% of parents prioritize “safe and non-toxic” first (NPD Group).
- Learning outcomes: tactile and physical product attributes influence perceived quality; children using tactile tools have shown better retention versus screen-only learning (Journal of Educational Psychology), so color fidelity supports perceived learning value.
Essential categories of evidence suppliers must provide
-
Master sample and written approval
Signed, physical master samples (lab dip or molded color part) with buyer approval create the contractual reference. Suppliers should keep the approved master in production records and provide high-resolution photos under controlled lighting.
-
Instrumental color measurements
Spectrophotometer reports in CIE L*a*b* with measurement conditions (illuminant D65 or D50, 2° observer) and calculated Delta E values (ΔE2000 preferred). Provide average, minimum, and maximum ΔE for the batch compared to the approved master and show measurement locations on the part.
-
Defined tolerances and capability data
Specify acceptance criteria such as ΔE ≤1–2 for critical brand colors and ΔE ≤3 for non-critical components. Supply Statistical Process Control (SPC) charts and capability indices (Cp, Cpk) demonstrating consistent process performance—ideally Cpk ≥1.33.
-
Raw material and pigment traceability
Pigment supplier lot numbers, masterbatch records, resin lot IDs, and MSDS/Chemical Certificates. For toys, include evidence of restricted-substance testing (EN71-3, CPSIA limits, REACH SVHC free) linked to colorant lots.
-
Color fastness and durability tests
Provide test reports for lightfastness, abrasion/rubbing resistance, wash or wet rub (where applicable), and accelerated aging. Include pass/fail criteria and specimen photos pre/post-test.
-
On-site measurement protocol & GR&R
Document the measurement procedure, instrument model, calibration status, and a Gauge Repeatability & Reproducibility (GR&R) study to prove measurement reliability across operators and devices.
-
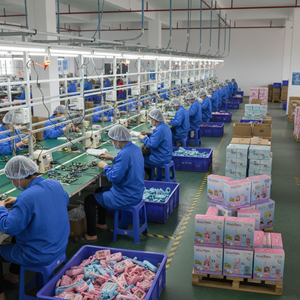
Production monitoring evidence
In-line check logs (start/mid/end of run) with sample IDs and spectrophotometer results, plus corrective action records when limits are breached.
-
Photographic and video evidence
Standardized, color-calibrated photos (include a color reference card in frame) taken at multiple production stages and during packaging.
How to structure acceptance criteria and process (recommended)
- Pre-Production: Request master samples, Pantone/Munsell/PMS numbers, and an initial spectrophotometer report.
- First Article: Approve lab dips or first molded parts with ΔE comparisons and signed approval.
- In-Process Controls: Require SPC charts and at least three spot-check measurements per 1,000 units (or per shift) showing ΔE stays within agreed tolerance.
- Pre-Shipment: Receive final batch color report, production photos, pigment lot traceability, and chemical compliance certificates.
- Audit Rights: Contractual right to audit supplier production and lab records for high-volume or brand-critical components.
Quick checklist for buyers to request from suppliers
- Signed master sample + digital color code (Pantone/Munsell) and ICC profile
- Spectrophotometer L*a*b* reports with ΔE2000 values and measurement settings
- SPC charts, Cp/Cpk values, and GR&R results
- Pigment/resin lot numbers and MSDS/COA
- EN71/CPSIA/REACH related test reports where color chemistry is involved
- Visual photos with color card and time-stamped production images
Comparison: Evidence Tiers for Color Control
| Tier | Instrument Reports | Pigment Traceability | SPC & Capability | Fastness/Chemical Tests | Best for |
|---|---|---|---|---|---|
| Basic | Single spectrophotometer read per batch (L*a*b*) | Supplier lot IDs | No Cp/Cpk; manual spot checks | Basic safety COA | Prototypes, low-volume SKUs |
| Standard | Multiple reads, ΔE2000 avg/max, measurement protocol | Masterbatch traceability + MSDS | SPC charts; Cp≈1.0–1.33 | EN71/CPSIA spot tests as required | Mass-market components, color-important SKUs |
| Premium | Full spectro reports, GR&R, ICC & Pantone mapping | Full lot traceability + COA per pigment lot | Cp/Cpk ≥1.33, SPC with automated in-line checks | Comprehensive fastness & migration tests | Brand-critical colors, private-label lines |
Implementation tips for buyers
- Define ΔE acceptance numerically in PO/QA agreements; avoid vague terms like “color must match.”
- Require suppliers use calibrated instruments and share raw measurement files (CSV) — this reduces disputes.
- Include color clauses in contracts permitting third-party lab verification and holdback for non-conforming batches.
- For toys, combine color evidence with chemical testing because colorants can affect compliance with EN71/CPSIA.
What Delta E value should I accept for toy parts?
Accept ΔE2000 ≤1–2 for critical brand colors and ≤3 for non-critical components. Agree tolerance per SKU in writing and require SPC evidence from the supplier.
Which measurement conditions should reports include?
Reports should state instrument model, illuminant (D65 or D50), observer angle (2°), geometry (e.g., 45/0 or sphere), aperture size, and calibration status.
How do I verify pigment safety and regulatory compliance?
Request pigment lot numbers, MSDS, Certificate of Analysis, and relevant test reports (EN71-3, CPSIA lead and heavy metals limits, REACH). Link these documents to the specific production batch.
Is photographic evidence reliable for color approval?
Photographs help but are not sufficient alone. They must be color-calibrated with a reference card; combine photos with spectrophotometer data and physical master samples.
What operational controls can suppliers show to prove consistency?
Look for SPC charts, start/mid/end production measurements, Cp/Cpk values, corrective action logs, and GR&R studies proving repeatable measurement.
Ready to Source from Toyvao?
Contact us today for factory-direct pricing, OEM/ODM customization, and fast global shipping.
WhatsApp: +86 186 8106 4480
Email: sales@toyvao.com
Website: toyvao.com