How Should Importers Assess Card-Size Tolerance Before Mass Production?
Accurate card-size tolerance assessment prevents costly rework, rejects, and compatibility failures for products such as flash cards, OID reading cards, and wearable anime badges. For importers and brand owners, a structured tolerance-validation process protects margins and brand reputation before scaling to full production.
Why tolerance matters in children’s educational products
Card and component dimensions determine device compatibility (e.g., OID pens and sensor alignment), packaging fit, and user safety. The global educational toy market is projected to reach $34.5 billion by 2028 (CAGR 9.5%) — reinforcing the pressure to deliver reliable, compliant products at scale (Grand View Research). Meanwhile, parents prioritize safety and non-toxicity — 73% name it their #1 criterion when buying toys (NPD Group) — so dimensional control often ties into safety features and pass/fail criteria during certification.
Common failure modes caused by poor tolerance control
- Misaligned touch/contact points in card readers (lost functionality)
- Cards jammed in dispensers or sleeves (mechanical failures)
- Bulged or deformed cards after lamination or coating (appearance and durability issues)
- Rejected lots due to AQL failure or safety certification nonconformance
Step-by-step: Assess card-size tolerance before mass production
- Define functional critical dimensions (FCDs). Map all dimensions that affect functionality: card length/width/thickness, corner radius, hole placement, printed OID grid alignment, and any embedded electronic placement.
- Set specification bands and nominal values. Use device requirements and manufacturing capabilities to set realistic tolerances (e.g., ±0.3 mm for printed cardstock, tighter for PVC smart cards). Include GD&T callouts for orientation and flatness where necessary.
- Conduct material-specific shrinkage checks. Paper, board, PVC, and PET shrink or swell under heat/humidity; laminate and coating layers add thickness. Measure pre- and post-process samples to quantify dimensional drift.
- Prototype and tool try-out. Produce pilot dies, mold inserts, or small injection runs. Use these to evaluate die-cutting creep, mold shrinkage, and tool wear—adjust tooling before committing.
- Implement measurement methodology. Select calibrated instruments: digital calipers for thickness, optical comparators for profile and corner radii, CMM or vision systems for multi-feature inspection, and go/no-go gauges for high-speed acceptance checking.
- Run tolerance stack-up and failure-mode analysis. Model how individual tolerances accumulate in assembly and interaction with the device. Prioritize tighter control on features that multiply error downstream (e.g., OID dot placement relative to card edge).
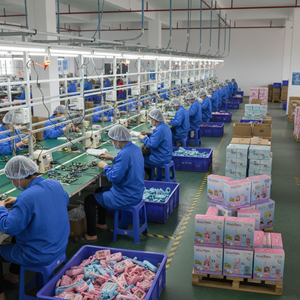
- Pilot batch inspection and AQL sampling. Produce a pilot batch representative of full production. Inspect per an agreed sampling plan (AQL/ISO 2859) and record SPC data for continuous improvement.
- Define vendor acceptance criteria and change control. Lock in tolerance drawings, inspection methods, and corrective action timelines in the purchase order and PPAP-like documents for toys and components.
Measurement tools and inspection best practices
- Use calibrated digital calipers (0.01 mm resolution) and thickness gauges for card body checks.
- Optical measurement or vision systems for pattern alignment (OID patterns require sub-millimeter accuracy).
- CMM for molded or plated parts with embedded electronics (e.g., wearable badges).
- Go/no-go gauges for assembly-critical features on production lines to speed acceptance.
- Record SPC charts and use control limits to detect drift early.
Supplier selection and dossier items to request
When evaluating suppliers, require: detailed tolerance tables, tooling maintenance plans, sample PPAP, calibration certificates for inspection equipment, and an inspection plan aligned with your AQL. For electronic badges and cards with embedded components, also request ESD, RoHS, and material safety test reports — aligning with the fact that global wearable technology is scaling fast (Statista projects the market reaching $186 billion by 2030), and component reliability is mission-critical.
Cost vs. tolerance: balancing quality and price
Tighter tolerances increase tooling, inspection, and scrap costs. Prioritize tight tolerances only where function or safety demands it. For marketing-focused aesthetics or non-critical features, relax tolerances to optimize cost. Document decisions and include them in supplier contracts to avoid disputes during volume runs.
Case example: Talking flash cards and OID reading cards
Toddler flash cards (paperboard): typical size 90 x 60 mm with recommended tolerance ±0.5 mm for length/width and ±0.1 mm for thickness post-lamination. OID reading cards require dot-grid alignment within ±0.3 mm to maintain reliable pen recognition. Children who use tactile learning tools show 40% better retention vs screen-based learning, so preserving tactile quality (flatness, edge finish) is also a functional requirement (Journal of Educational Psychology).
Practical checklist for importers (before mass run)
- Approve engineering drawings with GD&T callouts
- Validate materials and suppliers’ calibration certificates
- Run pilot production and record SPC
- Confirm tooling adjustments after try-out
- Sign off on AQL sampling plan and inspection methods
- Include remedial warranty and rework clauses in contracts
Comparison: Recommended tolerances by product type
| Product Type | Typical Nominal Size | Recommended Tolerance | Critical Features | Inspection Method | Relevant Certification |
|---|---|---|---|---|---|
| Paper Flash Cards | 85–100 x 55–70 mm | ±0.5 mm (L/W), ±0.1 mm (thickness) | Edge square, lamination flatness | Calipers, optical comparator | ASTM F963 / EN71 (material safety) |
| OID Reading Cards | Various (grid-based) | ±0.3 mm (dot alignment), ±0.3 mm (L/W) | OID grid placement, print registration | Vision system, template jigs | EN71, RoHS (ink/PCB) |
| PVC Smart Cards / Badges | ISO credit-card size or custom badges | ±0.15 mm (L/W), ±0.05 mm (thickness) | Edge radius, chip position | CMM, calipers | RoHS, REACH |
Final recommendations for importers
Do not treat tolerance as a one-off checklist item. Integrate tolerance strategy into product design, supplier selection, and quality control plans. With China exporting over $38 billion in toys annually (China Customs), strong pre-production validation ensures you capture the advantages of competitive Chinese manufacturing while avoiding common pitfalls that lead to delays and chargebacks.
What tolerance should I specify for laminated paper flash cards?
Specify ±0.5 mm for length/width and ±0.1 mm for thickness after lamination; validate with pilot runs since lamination can add thickness and cause minor shrinkage.
How do I verify OID dot alignment before mass production?
Use a vision inspection system or precision template to measure dot positions relative to card edges; require supplier to provide sample runs and SPC data demonstrating sub-0.3 mm repeatability.
What inspection frequency should I require for long runs?
Implement SPC with hourly sampling for key features during the first production shift, then adjust to regular lot-based sampling (AQL) once the process is stable.
Can tighter tolerances improve product safety?
Yes—critical dimensional control can prevent mechanical failures and choking hazards from ill-fitting parts; combine dimensional controls with material safety tests to meet parental safety expectations.
Is tooling try-out necessary for card products?
Always run tooling try-outs. Tooling wear and process variables often require iterative adjustments to meet tolerance bands and avoid costly post-production corrections.
Ready to Source from Toyvao?
Contact us today for factory-direct pricing, OEM/ODM customization, and fast global shipping.
WhatsApp: +86 186 8106 4480
Email: sales@toyvao.com
Website: toyvao.com