Choosing a custom housing color for electronic flash card readers is more than an aesthetic decision — it affects manufacturability, regulatory compliance, user perception, and cost. Importers who verify color accuracy and Pantone matching up front reduce delays, avoid costly rework, and protect brand reputation.
Why precise color matching matters for flash card readers
Flash card readers are tactile educational products that sit at the intersection of toy safety, product design, and consumer trust. With the global reading pen market growing at an estimated CAGR of 8.2% through 2027, competition increasingly hinges on product finish and consistent color across production runs. Consistency in housing color signals quality to distributors and end consumers — and aligns with safety and material requirements that 73% of parents cite as their top buying priority: “safe and non-toxic.”
Immediate commercial risks of poor color control
- Retail returns and chargebacks when visible color shifts reach customers
- Delay in shipments due to rework, repainting, or rejected lots
- Brand damage from mismatched SKUs and inconsistent packaging
- Regulatory non-compliance if pigments or coatings contain banned substances
Key technical aspects importers must verify before ordering
-
Pantone specification and substrate note
Confirm the exact Pantone (PMS) code and specify whether it is Solid Coated, Solid Uncoated, or a Textile/Specialty library. Because plastics and paints render color differently than paper, the Pantone reference must include the intended substrate (e.g., ABS injection molding vs. sprayed acrylic).
-
Material & coloring method
Decide injection-color masterbatch (colorant added to plastic), painted/coated finish, or film-wrapped. Each method affects color tolerance, durability, and cost. For example, color-added plastics eliminate peeling but can show batch-to-batch variance if masterbatch control is weak; painted finishes enable metallics and gradients but introduce adhesion and VOC considerations.
-
Acceptable color tolerance (Delta E)
Set a Delta E target up front. Industry practice: ΔE ≤ 2 is acceptable for consumer electronics; ΔE ≤ 1 is ideal for premium brands. Require supplier-supplied spectrophotometer readings measured under D65 illumination and 10° observer angle.
-
Finish specification: gloss, texture, and coating
Specify gloss units (GU) for shiny vs. matte finishes and any texture or soft-touch requirements. Provide photos plus numeric targets so production and QA teams have objective checks.
-
Color fastness and environmental testing
Mandate tests for UV resistance, abrasion, sweat, and chemical exposure. This is crucial for toddler products and for countries with intense sunlight.
-
Regulatory and safety compliance
Ensure pigments and coatings comply with RoHS, REACH, EN71 (where applicable), and any client-specific restricted substance lists. With China’s toy export value exceeding $38 billion annually, many factories are experienced in meeting these global standards, but you must request certificates and lab reports.
Step-by-step color approval workflow to include in your purchase order
- Submit Pantone code(s), material type, and finish spec with PO.
- Request factory to issue a physical Pantone chip and a master sample (first article) mailed to your QC team or third-party inspector.
- Approve pre-production sample (PPS) with spectrophotometer readings (ΔE value included) and photos in standard lighting (D65).
- Lock color recipe and sign off on a color run sheet that the factory must follow for production batches.
- Perform First Article Inspection (FAI) on initial shipment, checking ΔE, gloss, adhesion, and safety tests.
Documentation and test reports to request
- Material specification sheet and masterbatch recipe
- Spectrophotometer reports (ΔE values) vs. approved sample
- Photos under controlled lighting (D65) and a physical master sample
- Coating and paint MSDS (safety data sheets) and VOC emission reports
- Third-party lab reports for RoHS/REACH/EN71 or relevant standards
Common manufacturing pitfalls and how to prevent them
- Metamerism: Colors that match under one light source but differ under another. Mitigate by specifying D65 and viewing under multiple lamps.
- Incorrect Pantone library: Paper vs. plastic references produce different results. Always state substrate and provide a plastic master sample.
- Insufficient color control in production: Require the supplier to use a single masterbatch lot per order and maintain color run records.
- Failure to test final coated parts: Always test finished housings (not raw pellets) for adhesion and abrasion.
Comparison: Color control tiers for electronic flash card readers
| Tier | Method | Delta E Target | Typical Lead Time | Certifications/Tests |
|---|---|---|---|---|
| Standard | Injection color masterbatch | ΔE ≤ 3 | 4–6 weeks | RoHS basic, MSDS |
| Enhanced | Painted finish with UV topcoat | ΔE ≤ 2 | 6–8 weeks | RoHS, REACH, adhesion, UV test |
| Premium OEM | Masterbatch + specialized coating (soft-touch/metallic) | ΔE ≤ 1 | 8–12 weeks | RoHS, REACH, EN71, third-party lab reports |
Practical checklist for your sourcing team
- Include Pantone code and substrate in the PO.
- Require a mailed physical master sample and spectrophotometer report.
- Specify ΔE acceptance criteria and gloss units.
- Mandate RoHS/REACH/EN71 documentation and MSDS for coatings.
- Request factory color run sheets and traceability per batch.
- Budget for pre-production sampling and possible rework to avoid larger costs later.
Closing note
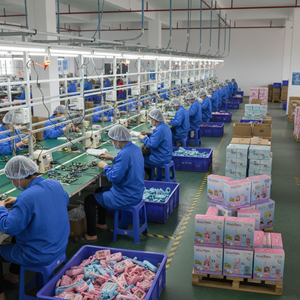
Tight color control is a competitive advantage for distributors and brands of electronic flash card readers. With careful specification, objective measurement, and a documented approval workflow you can avoid common quality failures, protect end-customer trust, and maintain cost predictability. Factories in Shenzhen such as Toyvao are experienced with OEM/ODM color processes for child-focused electronics — pair that expertise with strict PO terms and the right tests to deliver consistent, safe products at scale.
What Delta E value should I insist on for consumer-grade flash card readers?
For consumer-grade products, require ΔE ≤ 2 as an acceptable tolerance; set ΔE ≤ 1 for premium SKUs. Include spectrophotometer reports measured under D65 lighting.
Should I use painted housings or colored plastic for toddlers’ devices?
Colored plastic (masterbatch) resists peeling and is durable, but painted finishes allow special effects. For toddlers’ devices prioritize safety and adhesion tests; if using paint, request EN71/REACH-compliant coatings and adhesion/abrasion results.
How do I avoid metamerism problems?
Specify D65 lighting and require color approval under multiple light sources. Approve a physical master sample rather than relying solely on printed Pantone chips.
What documentation should accompany a color approval?
Require a physical master sample, spectrophotometer ΔE report, material MSDS, and any third-party compliance reports (RoHS/REACH/EN71) for coatings or pigments.
How do manufacturing costs change with tighter color tolerances?
Tighter tolerances (ΔE ≤ 1), specialty coatings, and additional testing increase upfront costs and lead times, but reduce rework, returns, and brand risk—often paying off in higher margins and fewer quality incidents.
Ready to Source from Toyvao?
Contact us today for factory-direct pricing, OEM/ODM customization, and fast global shipping.
WhatsApp: +86 186 8106 4480
Email: sales@toyvao.com
Website: toyvao.com