Importers sourcing educational or promotional cards (flash cards, game cards, wearable badge inserts) must verify card performance for dirt resistance and bending durability before committing to mass production. Early, methodical testing reduces rejects, protects brand reputation, and aligns with global safety expectations for children’s products.
Why pre-production testing for dirty or bent cards matters
Cards that attract dirt, smudge, or permanently deform in transit lead to higher return rates, customer complaints, and waste. For children’s learning products — where tactile quality directly affects engagement — reliable physical performance is a competitive requirement. The global educational toy market is projected to reach $34.5 billion by 2028 (CAGR 9.5%), and many importers choose Chinese manufacturing because China exports over $38 billion in toys annually; both facts underline why rigorous pre-production QC in China is pivotal for global brands.
Key commercial risks from dirty or bent cards
- Rejected consignments at retail or distribution centers (costly delays, rework).
- Damaged brand equity when cards look used or low-quality on shelves.
- Product malfunction in card-fed devices (jams, misreads) causing returns.
- Non-compliance with child-safety expectations — 73% of parents rank “safe and non-toxic” first when buying toys.
Step-by-step assessment protocol before mass production
Use the following practical sequence to evaluate dirty and bent card performance. These steps combine simple in-factory checks and small-scale lab tests.
- Define acceptance criteria up front
Agree with your supplier on measurable criteria: visual cleanliness (no visible particles or stains under 5–10x loupe), lamination adhesion (no lift after 20 rubs), bend recovery (no permanent deformation after X cycles), and feed reliability in your device. Use AQL sampling plans (critical level for children’s products is typically AQL 2.5).
- Material and print verification (incoming raw materials)
Request datasheets for paper/cardstock GSM, coating type, and lamination film specs. Check for hydrophobic coatings or anti-static finishes that reduce dirt attraction. Ask for Certificates of Analysis (COA) and material supplier traceability.
- Pre-production sample run
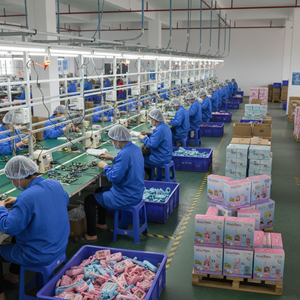
Produce a pilot batch (200–1,000 cards depending on SKU complexity). Run these through the full manufacturing sequence: print, coat, laminate, die-cut, edge finish, and pack. Inspect every process step for contamination sources (rollers, dust on platens, operator gloves).
- Environmental conditioning
Expose sample cards to typical shipping/storage humidity and temperature cycles for 72 hours. Humidity can cause curl, delamination, and increased dirt adherence — assessing performance after conditioning simulates real-world distribution.
- Bend and flex testing
Perform manual and machine-based bend tests: repeated 90° folds at the corner and center, flex cycles (500–2,000) depending on expected life, and a one-time crease test to detect permanent deformation.
- Abrasion and rub tests for dirt/smear
Use a simple rub test (cloth or machine) to simulate handling and wallet/pocket abrasion. Check for ink migration, laminate scuffing, and dirt pickup. If cards are used with devices (card feeders, badges), cycle them through the device to test for jamming or read errors.
- Quantify and document results
Log failures by defect type and severity, and produce a remediation plan with the supplier (material change, tighter process controls, surface treatment). Retest after corrective actions before approving full tooling and mass production.
Practical checklist for on-site inspectors
- Confirm paper/cardstock GSM and coating specification match approved sample.
- Inspect 10% of pilot run visually and under 5–10x loupe for particulate contamination, glue bleed, or scuffs.
- Run 100 cards through intended device(s) to confirm feed reliability.
- Perform 20 rub/abrasion cycles on multiple card locations.
- Condition sample packs at 30–80% RH and repeat visual and bend tests.
- Verify packaging protects edges (corner protectors, sealed inner bags) and will not cause bending during transit.
Certification, documentation, and supplier requirements
Require your supplier to provide certificates relevant to toys and children’s products where applicable (EN71 parts, ASTM F963, REACH, RoHS, CPSIA test reports). Children who use tactile learning tools show 40% better retention vs screen-based learning, so product integrity matters both pedagogically and commercially. Document corrective action timelines and include clean-room practices or dust-control improvements in the production SOP if contamination is frequent.
Comparison: Card quality tiers for buyers
| Tier | Material (GSM) | Lamination / Finish | Dirt Resistance | Bend Tolerance | Certifications | Typical MOQ |
|---|---|---|---|---|---|---|
| Basic | 200–250 | Unlaminated / Matte | Low (prone to smudge) | Low (may crease after handling) | RoHS | 1,000 pcs |
| Standard | 250–300 | Single-side lamination / Gloss | Medium (some protection) | Medium (survives light flex) | RoHS, REACH | 500–2,000 pcs |
| Premium | 300–350+ (card stock) | Double-side lamination / Anti-smudge coating | High (hydrophobic / anti-static) | High (500–2,000 flex cycles) | EN71, ASTM, RoHS, REACH | 500 pcs+ |
Supplier selection and cost trade-offs
Higher upfront cost for premium materials and tighter process control reduces lifecycle cost from returns and rework. In the context of a growing educational toy market and adjacent categories (reading pen market growth CAGR 8.2% through 2027), investing in card durability is a way to differentiate products and secure retail partnerships.
Final recommendations
- Agree acceptance criteria and AQL levels in the contract before tooling or mass runs.
- Require pilot runs and documented retests after corrective actions.
- Include device-integration testing (feed/jam/read reliability) as part of sign-off.
- Insist on documented material traceability and relevant safety test certificates.
How many sample cards should I test before mass production?
Start with a pilot batch of 200–1,000 cards depending on SKU complexity and run AQL sampling (critical items often use AQL 2.5). Include device-feed tests and environmental conditioning in your sample protocol.
What are the easiest tests to detect dirt attraction?
Use a visual inspection under 5–10x loupe, a 20-cycle cloth rub test for smearing, and humidity conditioning to reveal dirt pickup. Check handling points like edges and printed areas for glue or ink transfer.
How do I evaluate bend or crease resistance?
Perform repeated 90° fold tests at corners and center, and run flex cycles (several hundred to thousands depending on expected use). Inspect for permanent deformation, laminate lift, or surface cracking.
Are there certifications that help guarantee card safety for children?
Yes. Relevant tests include EN71 (European toy safety), ASTM F963 (US toy safety), REACH and RoHS for chemical compliance, and CPSIA for lead/phthalates where applicable. Request lab reports from accredited labs.
Can packaging prevent bending and dirt during transit?
Appropriate inner packaging (sealed polyethylene bags, corner protectors, rigid trays) and outer carton bracing reduce bending and contamination. Validate packaging through a simulated transit test before full production.
Ready to Source from Toyvao?
Contact us today for factory-direct pricing, OEM/ODM customization, and fast global shipping.
WhatsApp: +86 186 8106 4480
Email: sales@toyvao.com
Website: toyvao.com